
60x Speed Unit Errors: Basswood Laser Test Grid (2026)
Confusing mm/s with mm/min creates a 60x speed error that can scorch basswood or produce a weak mark. This guide shows how to verify the unit, convert copied values, and run a simple unit-sanity ladder before using a production sheet.
By Mike Dolan ·
Quick Answer: A 60x unit mismatch can mimic bad power or focus, so convert every copied speed and verify it on a labeled basswood ladder first.
| Material | Engraving Contrast | Cut Ease | Smoke / Odor | Cost | Beginner Score |
|---|---|---|---|---|---|
| Basswood (3 mm) | ★★★★★ | Excellent — 1 pass | Low | $ | ★★★★★ |
| Baltic Birch Plywood | ★★★★ | Good — 2–3 passes | Medium | $$ | ★★★★ |
| MDF | ★★★ | Good — 1–2 passes | High (formaldehyde) | $ | ★★ |
| Pine / Soft Plywood | ★★★ | Poor — resin deposits | Medium-High | $ | ★★ |
Why Even Basswood Makes a Speed Ladder Easy to Read
Consistent 3mm basswood makes a unit-sanity ladder easy to read: even color and density help a 2x speed change show clearly. A $2.08 scrap sheet is cheap insurance compared with wasting a production sheet.
- Low resin — clean, even scorch so a change in speed shows up as a change in the mark
- Consistent density — each rung of the ladder reacts to speed, not to a hard or soft patch of grain
- Minimal char — differences between rungs stay easy to compare by eye
- Light, even color — a 2x speed change reads clearly against the pale surface
- Cheap scrap — a $2.08 sheet is inexpensive insurance before a production run
Why One Wrong Unit Becomes a 60x Error
One wrong speed unit creates a 60x error because mm/s and mm/min measure the same motion over different time periods. One mm/s equals 60 mm/min, so entering a value intended as mm/s into a mm/min field makes the laser move 60 times slower than expected.
Enter 10 as mm/min when the source meant 10 mm/s, and the real motion becomes about 0.17 mm/s. That can scorch or burn through basswood. Reverse the mistake and enter 600 as mm/s when the source meant 600 mm/min: the machine runs at 600 mm/s, or 36000 mm/min, leaving a weak mark or failed cut.
GRBL and LaserGRBL normally use mm/min for speed or the F word, so F200 means 200 mm/min. LightBurn can show speed per second or per minute depending on device configuration. Check the unit beside the speed field and in Device Settings, because menu wording can vary by version.
I once copied a bare forum speed, watched basswood turn dark almost immediately, and blamed focus first. The actual problem was simpler: the source used one unit and my software used another. Never assume a setting from another program uses the same speed unit as yours.
Laser Speed Conversion Cheat Sheet
Convert the copied value before entering it, then confirm the unit shown in your software field. These figures describe unit conversions only, not recommended machine settings. Inches are a separate unit, so convert them before entering a value into a field labeled mm/s or mm/min.
- mm/s to mm/min: multiply by 60.
- mm/min to mm/s: divide by 60.
- 10 mm/s = 600 mm/min.
- 600 mm/min = 10 mm/s.
- 10 in/min = 254 mm/min, about 4.23 mm/s.
I keep the unit written beside every copied speed before it reaches the laser software. That small habit catches the most expensive typo: a bare number that looks familiar, fits neatly in the field, and sends the head moving at a completely different rate.
The 3-Rung Unit-Sanity Speed Ladder
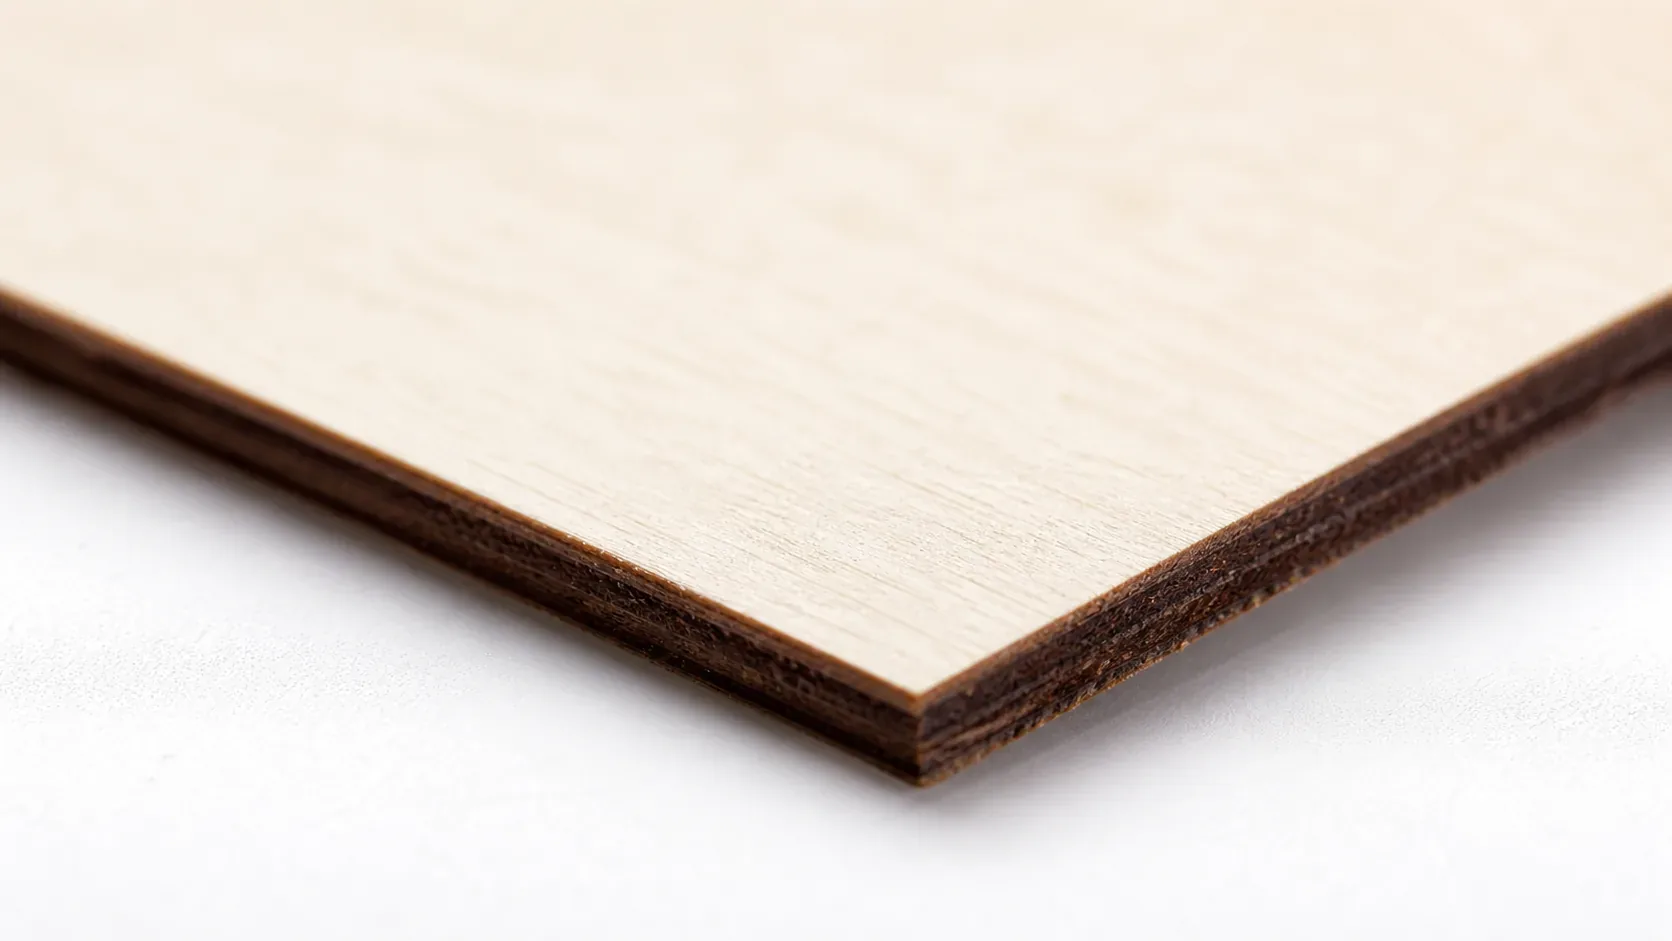
The 3-rung ladder checks whether your software is reading speed units as expected. On scrap 3mm basswood, keep power, focus, air assist, and pass count identical across every rung. The values below illustrate a doubling ratio only, not recommended settings for any machine.
- 2.5 mm/s = 150 mm/min.
- 5 mm/s = 300 mm/min.
- 10 mm/s = 600 mm/min.
Write the complete label on the scrap, such as 600 mm/min, never just 600. Each doubling of speed should visibly reduce char or burn depth compared with the slower rung. If the middle result looks extremely slow or fast, stop and inspect the displayed unit before continuing.
I label each rung before firing the job, because a clean-looking scrap sheet is useless if I cannot identify its unit later. Record the software, power, passes, material thickness, date, and exact speed with its unit. Keep every other condition unchanged so speed unit is the variable being checked.
Four Speed-Unit Mistakes That Waste Basswood
The four mistakes are copying unlabeled numbers, mixing units, trusting imported settings, and skipping a scrap ladder. Each one can turn a simple reference into charred basswood or a failed cut. The fix is not fancy: write the unit, inspect the field, and check behavior on scrap first.
- Copying a bare number: A speed without mm/s, mm/min, or in/min is a trap. Record the unit beside every value before copying it into laser software.
- Mixing units in one job: A test sheet cannot provide a meaningful visual comparison if its labels use different units, even when the numbers look tidy.
- Trusting an imported file or update: An imported file or software update can change how a value is interpreted. Inspect the speed field and device settings again.
- Skipping the scrap ladder: Going straight to a production sheet turns a quick unit check into wasted material. Run the ladder before committing a finished sheet.
I have caught unit confusion before it reached a production sheet by using the test card playbook and the laser calibration card guide. Those resources cover broader test-card work; this check stays focused on the mm/min versus mm/s sanity check.
Where to Get Basswood for Your Test Ladders
Crafteker 3mm basswood sheets are 12×12 inch, laser-grade, void-free, and pre-sanded – consistent enough that a speed change reads clearly on the wood instead of hiding in grain differences. At $24.99 for 12 sheets ($2.08/sheet), a few scrap rungs cost almost nothing next to a ruined production sheet.
Ready to test before you cut?
→ Buy Crafteker 12-Pack Basswood Sheets on Amazon – $24.99
Also available: 5-pack ($15.97) · 3-pack ($12.99)
Frequently Asked Questions
How do I convert mm/s to mm/min?
Multiply the mm/s value by 60. For example, 10 mm/s equals 600 mm/min.
How do I convert mm/min to mm/s?
Divide the mm/min value by 60. For example, 600 mm/min equals 10 mm/s.
What speed unit does LaserGRBL use?
GRBL and LaserGRBL normally use mm/min for the speed or F word. Check your own software display before entering a copied value.
Does LightBurn always use mm/s or mm/min?
No universal unit should be assumed. LightBurn can display speed per second or per minute depending on the device configuration, so check the unit beside the speed field and in Device Settings.
What should I do if a basswood rung looks badly burned or too weak?
Stop before changing machine settings. Check whether the typed number has the correct unit, confirm the conversion, inspect the label on the scrap, and repeat the unit-sanity ladder with the same test conditions.
About the author: Mike Dolan is a laser maker and wood materials specialist with 8+ years cutting basswood, birch, and MDF on diode and CO₂ machines. He tests every Crafteker basswood batch before listing.
I keep a marker beside the laser because a bare speed number is how good basswood becomes smoke. Writing 600 mm/min on the scrap and logging the software has saved me from repeating the same mistake.