
3mm Basswood Hardware Clearance Guide: M3/M4 Holes 2026
M3 clearance holes run about 3.4mm and M4 about 4.5mm for a normal fit in laser-cut 3mm basswood, and the actual finished hole always comes out smaller than what you drew because the laser eats a kerf width on the way through. This guide gives you the hole-sizing numbers for screws, Chicago screws, and key rings so your hardware slides in clean instead of fighting you at final assembly.
By Mike Dolan ·
Quick Answer: Screw-hole and hardware clearance guide for 3mm basswood: M3 holes run 3.2-3.6mm and M4 holes run 4.3-4.8mm depending on fit, then adjust further for your own machine’s kerf.
| Material | Engraving Contrast | Cut Ease | Smoke / Odor | Cost | Beginner Score |
|---|---|---|---|---|---|
| Basswood (3 mm) | ★★★★★ | Excellent – 1 pass | Low | $ | ★★★★★ |
| Baltic Birch Plywood | ★★★★ | Good – 2-3 passes | Medium | $$ | ★★★★ |
| MDF | ★★★ | Good – 1-2 passes | High (formaldehyde) | $ | ★★ |
| Pine / Soft Plywood | ★★★ | Poor – resin deposits | Medium-High | $ | ★★ |
The Standard M3 and M4 Clearance Hole Sizes for Laser-Cut Basswood
For a normal fit, M3 holes want to land at 3.4mm and M4 holes at 4.5mm. Drop to 3.2mm and 4.3mm for a close, snug fit, or open up to 3.6mm and 4.8mm when the screw needs to spin freely without catching on the wood.
These aren’t basswood-specific numbers I made up. They’re the same metric clearance hole standards machinists use for sheet steel and aluminum, and they hold up fine in laser-cut wood once you dial in your machine’s own kerf on top of them.
Use close fits when a screw threads into a captured nut and you don’t want play. Use normal for general assembly through washers. Use loose when the piece needs to pivot on the screw, or you’re not sure your kerf matches mine exactly.
I learned the nominal-diameter trap the hard way on an early batch of picture frame stands. I drew the hole at the exact nominal screw diameter, figured that counted as “precise,” and every screw jammed at the surface until I sanded each hole by hand. Nominal diameter is the screw’s spec size, not a hole size – clearance always goes on top of it.
Before you commit to a design, dial in your basswood laser cutting settings so your kerf stays consistent pass to pass, and start with stock that behaves the same way every sheet, like the best basswood sheets for laser cutting – otherwise these clearance numbers drift on you between batches.
Why Your Drawn Hole and Your Finished Hole Are Never the Same Size
Your finished hole always comes out smaller than the circle you drew, because the laser doesn’t just trace a line – it removes a strip of material on the way through. That missing strip is the kerf, and it eats into your hole from every side, not just one.
This is the same principle that governs tight finger joints and living hinges, just applied to round holes instead of straight edges. If you want the actual measuring and math behind kerf itself, that’s covered in our kerf compensation for laser-cut joints guide – worth a read if you’re chasing precision fits across a whole project, not just hardware holes.
For hole sizing, the practical fix is simple: draw the hole a little bigger than the clearance number you land on, roughly by however much your own machine’s kerf runs. Every laser is different – power, speed, lens condition, even the batch of wood – so there’s no universal number here. Cut a scrap test hole, measure it with a caliper, and you’ll know exactly how much your machine is eating on every job after that.
Chicago Screws, Binder Posts, and Key Ring Holes: Getting the Fit Right
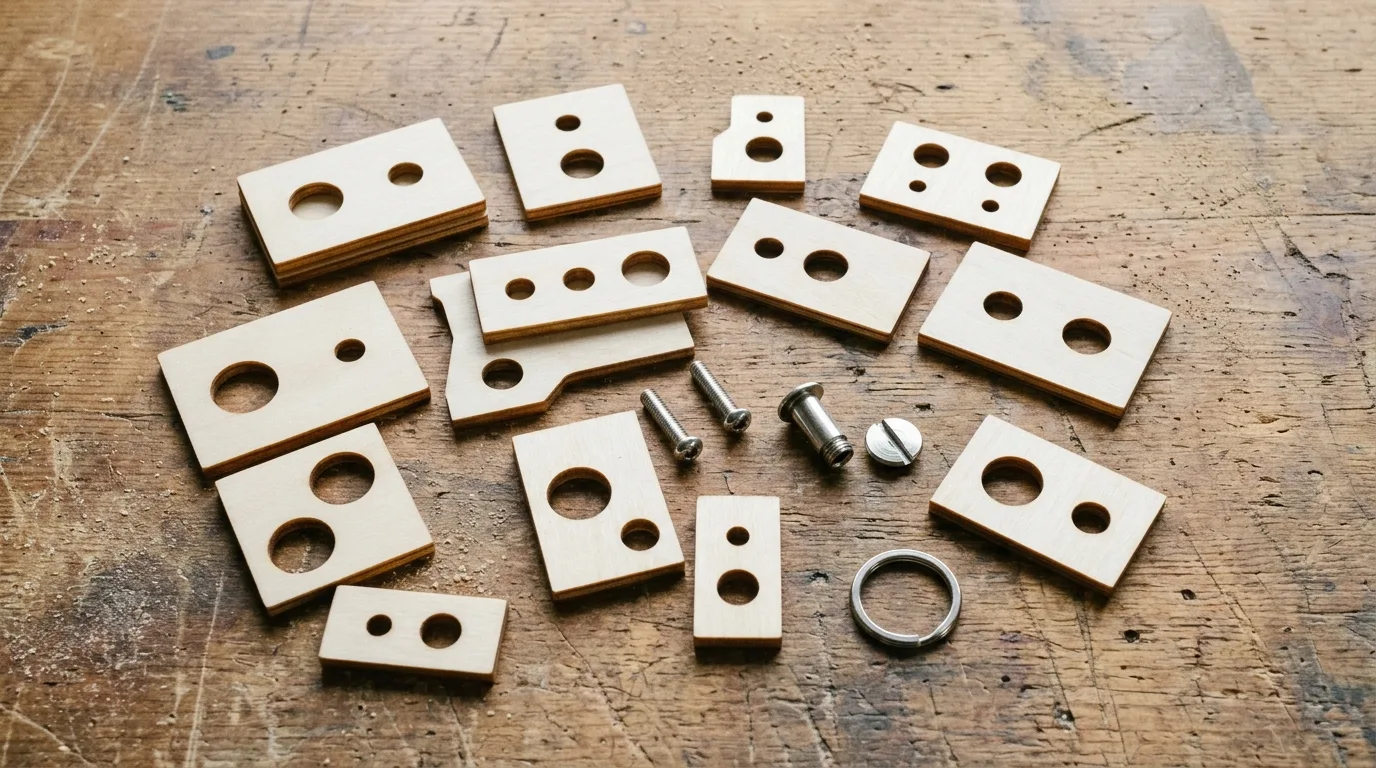
Chicago screws and binder posts need a hole sized to the barrel, not the screw’s nominal thread size – barrels typically run 4 to 5.5mm depending on the hardware you bought. Size the hole about 0.2 to 0.5mm larger than the barrel diameter and it’ll seat snug without binding when you thread the two halves together.
I once sized a batch of journal cover holes right at the barrel diameter with zero clearance, figuring snug was better than loose. Every single post jammed halfway in and I had to redrill the whole stack with a hand drill after the fact – not a fun afternoon. Give yourself that 0.2 to 0.5mm buffer up front and you skip that entirely.
Key ring holes in wood tags are a different animal and much simpler: a hole in the 3 to 4mm range clears most standard split rings and jump rings with room to spare. Don’t confuse that with the ring’s own diameter, which usually runs 20 to 30mm – that number is just reference for how the ring looks on the tag, it has nothing to do with what you drill.
Why Self-Tapping Screws Don’t Work Reliably in 3mm Basswood
No – 3mm just isn’t enough material for threads to grab and hold. A tap drill for M3 runs around 2.5mm and M4 around 3.3mm, and at that hole size in a sheet this thin, you’re left with maybe a turn or two of wood fiber doing all the work.
Those threads strip out fast, especially if you’re anywhere near an edge where there’s less wood to resist the screw pushing outward. I tried self-tapping near an edge on a test piece once and split it clean through – didn’t even get the screw fully seated.
Skip the threading entirely. Drill a clearance through-hole and back it with a nut and washer, or use a Chicago screw or binder post that clamps the layers together instead of biting into the wood.
A Quick Workflow for Sizing Any Hardware Hole
Run through this order every time and you’ll stop guessing at hole sizes:
- Identify the hardware: screw, Chicago screw/binder post, or key ring.
- Find its nominal or barrel diameter – check the packaging or measure with calipers.
- Add clearance: close/normal/loose for screws, or the barrel-plus-clearance rule for Chicago screws.
- Add your own machine’s kerf on top – see the kerf compensation guide for how to measure it.
- Test on scrap first. Always. Kerf shifts with power, speed, and even how sharp your focus is that day.
Dial in your cut quality too – a hole surrounded by char or fuzz behaves differently than a clean one. Our basswood laser cutting settings guide covers getting crisp edges before you even worry about hardware fit.
Why Crafteker Basswood Keeps Your Hole-Sizing Math Predictable
Because the sheet thickness doesn’t drift, so your kerf and clearance math from one batch carries over to the next. Crafteker basswood is 3mm, 12×12 inch, laser-grade, and void-free – no surprise density pockets throwing off a clean cut.
That consistency means you test your hole sizes once and trust them going forward instead of re-testing every new sheet. Available in 3-pack ($12.99), 5-pack ($15.97), or 12-pack ($24.99 – about $2.08 per sheet, the best value of the three).
Ready to cut? Get the wood that works with these settings:
→ Buy Crafteker 12-Pack Basswood Sheets on Amazon – $24.99
Also available: 5-pack ($15.97) · 3-pack ($12.99)
Frequently Asked Questions
What size hole do I need for an M3 screw in laser-cut basswood?
Roughly 3.2mm for a close fit, 3.4mm for a normal fit, or 3.6mm if you want the screw to drop in loose. Start with 3.4mm for most projects, then nudge up or down once you’ve test-fit a scrap piece and accounted for your own machine’s kerf.
What size hole do I need for an M4 screw in laser-cut basswood?
Roughly 4.3mm close, 4.5mm normal, or 4.8mm loose. Same logic as M3 – 4.5mm is the safe default for a snug-but-not-fighting fit, and you’ll still want to confirm it on scrap since kerf varies by machine, power, and speed.
Can I self-tap screws directly into 3mm basswood?
Not reliably. 3mm doesn’t give a self-tapping screw enough depth for real thread engagement, so the threads strip out fast and can split the wood, especially near an edge. Drill a clearance hole and back it with a nut and washer, or switch to a Chicago screw or binder post instead.
What size hole does a Chicago screw need in thin wood?
About 0.2 to 0.5mm larger than the barrel diameter, which usually runs 4-5.5mm depending on the screw you bought. That small bit of clearance is the whole trick – go too tight and you’ll be fighting binding, too loose and the post wobbles in the hole.
Where can I buy consistent 3mm basswood for hardware assembly projects?
Crafteker basswood on Amazon – 3-pack for $12.99, 5-pack for $15.97, or 12-pack for $24.99, which works out to $2.08 per sheet. Same thickness sheet to sheet means the hole-sizing numbers you dial in on one batch keep working on the next.
About the author: Mike Dolan is a laser maker and wood materials specialist with 8+ years cutting basswood, birch, and MDF on diode and CO₂ machines. He tests every Crafteker basswood batch before listing.
Redid a whole batch of keychain tags because I sized the holes to the exact ring wire diameter and nothing would thread through cleanly. Switched to the close/normal/loose clearance approach and ran a scrap test cut first for kerf, and the fit’s been consistent ever since – the Crafteker sheets being the same thickness pack to pack made that math actually hold up.